Agricultural Machinery Knowledge Series
What Is a Bale Wrapper Integration System
and How Does It Save Time?
A complete guide to understanding the mechanics, materials, and operational benefits of integrating a round baler with an automatic wrapping unit — and why farms worldwide are adopting this dual-function approach.
1. Understanding the Basics: What Exactly Is a Bale Wrapper Integration System?
A bale wrapper integration system is the mechanical and electronic connection that links a round baler’s compression and ejection sequence directly to a bale wrapping unit, allowing both processes to operate as a single workflow rather than two separate field passes. In traditional forage harvesting, operators would first complete all baling across a field, then follow up with a dedicated wrapper machine to apply stretch film or net around each bale. While functional, this two-pass method demands more time, more fuel, and more labor — a significant constraint during the narrow harvest windows that define silage season.
The integrated approach addresses that constraint head-on. Once a round baler finishes forming and binding a bale, a built-in transfer arm or conveyor moves it immediately to a turntable or satellite wrapper attached directly to the rear or side of the baler chassis. Film or net is applied on the move — or during a brief pause — before the wrapped bale is deposited on the field. The operator never leaves the cab. Total time from grass pickup to sealed bale can drop by 40–60% compared with operating separate machines.
This matters considerably for South Korean livestock and dairy farms, where labor availability is declining and the silage window — particularly for Italian ryegrass and whole-crop maize — can be as short as five to seven days. An integrated system turns every operational minute into productive output, which is why demand for capable round baler machines with wrapping capability has grown steadily across the Korean agricultural sector.
2. Action Mechanism: How the System Moves from Baling to Wrapping
The action sequence in an integrated bale wrapper system follows a logical chain that begins the moment the bale density sensor signals completion. In a variable-chamber round baler, the compression rollers and drum assemblies rotate until the bale reaches the pre-set diameter — typically between 1,000 mm and 1,400 mm depending on the model configuration. Once triggered, the binding mechanism engages automatically. In net-wrap systems, a motor-driven net feeder applies wrap across the full bale width in one or two revolutions, then cuts cleanly. The rear tailgate then opens hydraulically, and the formed bale rolls onto a transfer cradle.
The wrapper stage uses one of two principal mechanisms. A satellite-arm wrapper rotates two film rolls around a stationary bale, applying overlapping layers rapidly. A turntable wrapper spins the bale itself on a rotating platform while fixed film dispensers apply tension-stretched film from above. Both designs achieve the oxygen-tight seal necessary for fermentation. The turntable approach is typically found on trailed combination machines, while the satellite design is common in self-loading integrated units where speed is the priority.
Power flow throughout this system runs from the tractor’s PTO shaft at 540 rpm through the baler’s own gearbox, then via a secondary hydraulic circuit to the wrapper components. The hydraulic circuit controls tailgate opening speed, cradle tilt angle, and wrapper rotation speed. Modern integrated systems connect all these circuits through an electronic control unit (ECU) mounted in the cab, allowing the operator to monitor bale count, film consumption, and pressure settings from a single display without stopping.
3. Manufacturing Structure: How Integration Systems Are Built
The structural engineering behind an integrated bale wrapper system must solve a difficult balance: the wrapping unit adds significant weight and moment to the rear of the baler, yet the combined machine still needs to follow undulating terrain without binding or twisting. Most manufacturers solve this with a floating hitch or pendulum coupling between the baling section and the wrapping platform. This allows the two sections to articulate independently over ridges and dips while maintaining a rigid power transmission path.
Frame materials are predominantly high-strength structural steel, often S355 or equivalent grade, laser-cut and robot-welded for dimensional accuracy. The baler drum assembly and side cheeks — which experience the highest cyclic stress — are typically fabricated from 8–12 mm plate with reinforced corner gussets. Wrapper turntable frames, by contrast, prioritize low rotational inertia and are often manufactured from thinner, higher-grade steel to reduce mass while maintaining the torsional stiffness needed for reliable film tension.
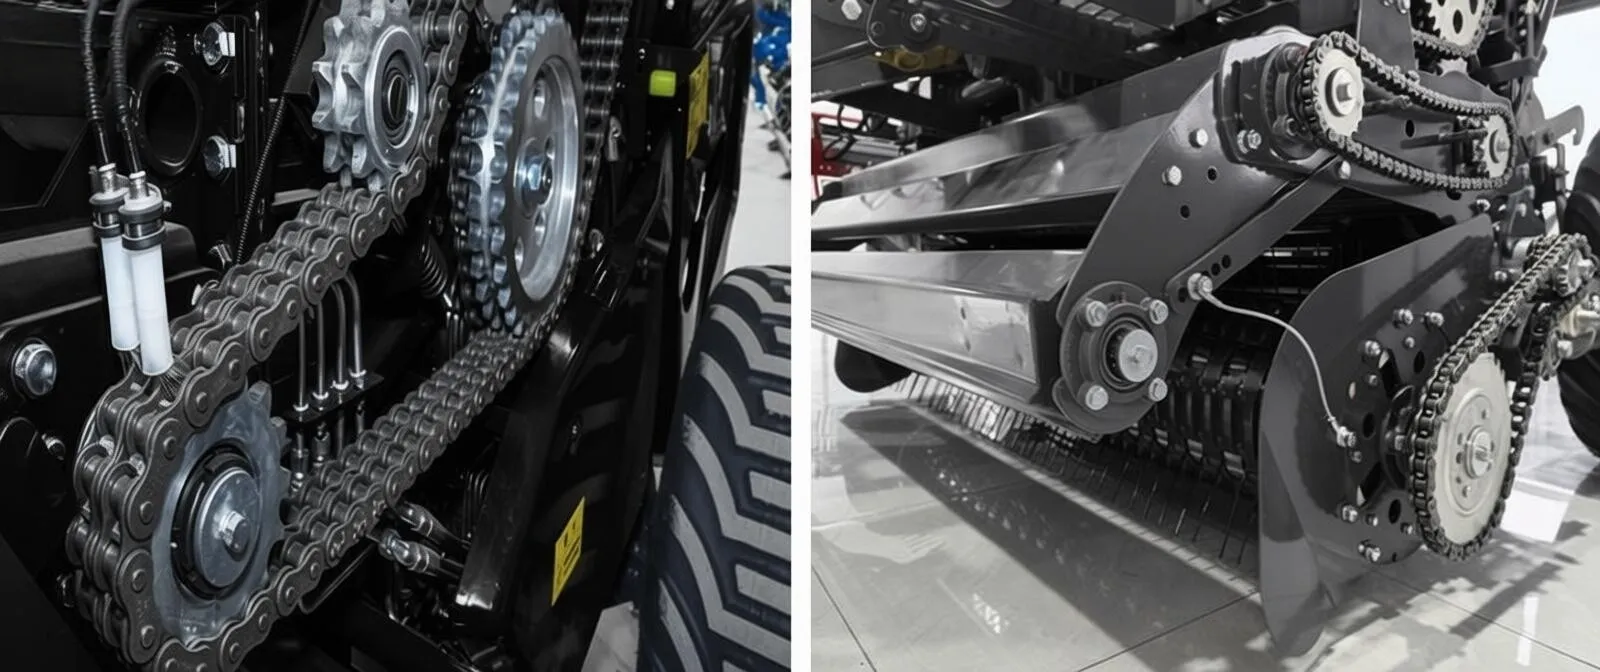
Chain and sprocket drive assemblies within the baler section use hardened-tooth 20A or 20B heavy-duty roller chains, especially in larger machines. In the 9YG-2.24D round baler, dual-sided 20A heavy chain in the rear chamber compartment increases compression force and enables bale densities consistently reaching 500–1,000 jin (approximately 250–500 kg). That density level is directly relevant to whether silage fermentation proceeds correctly — loose bales admit oxygen and risk spoilage, while overly compact bales can restrict proper anaerobic respiration of the plant material.
Key Structural Components
| Component | Function | Typical Specification |
|---|---|---|
| Compression chamber | Forms and compacts the bale | 18 rollers, φ222 mm roller diameter |
| Pickup header | Collects windrows from the field | Spring-tine type, 2,240 mm width |
| Feed roller / rotor | Channels material into chamber | Axial-flow semi-forced feed (patented) |
| Net-wrap dispenser | Applies binding net before ejection | Auto-wrap, 2,000 × 1.4 m per bale |
| Hydraulic tailgate cylinder | Opens rear door for bale ejection | H-type compression fitting, higher pressure rating |
| Wrapper transfer arm / cradle | Moves bale from baler to wrapper | Hydraulically operated, tilt-adjustable |
| Stretch film unit | Applies airtight film for silage | 500 mm film, 50–70% stretch, min. 4 layers |
| ECU control panel | Coordinates all integrated functions | Cab-mounted, 12V DC, sensor-linked |
4. Material System: What the Wrapper Actually Uses
The wrapping material in an integrated system is almost universally low-density polyethylene (LDPE) stretch film, typically between 25 and 35 microns thick, formulated with UV inhibitors and tackifiers. The tackifier causes successive film layers to bond to each other rather than sliding, which is essential for achieving the oxygen barrier needed for lactic acid fermentation. Without proper tackiness, small gaps between layers allow air infiltration that converts high-quality silage into spoiled fodder within days.
Most agronomic guidelines recommend a minimum of four overlapping film layers, with six layers for longer-term storage or in warmer climates. At a 50–70% stretch ratio, a 500 mm wide film roll can cover a standard 1.2–1.4 m wide bale effectively with each pass. The number of complete turntable or satellite revolutions is adjusted via the ECU to ensure full coverage from shoulder to shoulder, including the curved end faces which are often the weakest point in the oxygen seal.
Net wrap — the binding applied inside the baler before ejection — uses polypropylene (PP) or HDPE knotted or woven mesh with a typical tensile strength of 800–1,200 N per 200 mm strip. Its primary role is to hold the bale’s shape during ejection and transfer, not to provide a silage seal. The net allows some air exchange, which is why plastic stretch film wrapping follows immediately after in silage applications. For dry hay bales that will not be fermented, some farmers stop at the net-wrap stage and skip outer film entirely.
Twine binding — traditionally sisal or polypropylene twine — remains common in smaller round balers and in regions where net-wrap consumable costs are a factor. Twine-bound bales are somewhat less dense and less consistent in shape than net-wrapped ones, and they are generally unsuitable for silage applications due to the air gaps between twine strands.
5. How Does the Integration Actually Save Time in Practice?
The time argument for integrated systems is most compelling when you account for the full harvest chain rather than just machine cycle time. In a traditional two-machine operation, the baler and the wrapper run on separate schedules — the baler must finish all its passes before the wrapper can begin, or a second operator and tractor must follow behind in real time. Either way, the wrapper introduces a bottleneck that can delay silage sealing by several hours. Every hour of delay after cutting increases dry matter losses and reduces fermentation quality, particularly for wilted crops.
An integrated system eliminates this bottleneck entirely. Wrapping occurs within seconds to a few minutes of bale formation. For silage crops, reaching an oxygen-free environment quickly is not just a convenience — it is a quality imperative. Korean agricultural extension research indicates that delaying wrapping of wilted grass by even two hours under warm conditions can increase aerobic deterioration losses by 3–5% of dry matter, which translates directly into lower livestock performance through the winter feeding period.
On a practical throughput basis, a well-calibrated integrated combination machine can produce 40–100 wrapped bales per hour on open terrain, depending on windrow density and tractor power. That figure is comparable to running a high-output dedicated baler, yet eliminates the second field pass entirely. For Korean livestock operations typically managing 10–50 hectares of forage per season, the labor-hour saving over a full silage season is substantial.
Fewer field passes
Baling and wrapping in one trip cuts total field time by 40–60% compared with separate machines.
Faster sealing
Wrapping within minutes of bale formation preserves silage quality and reduces aerobic losses.
Single operator
One driver handles the entire bale-wrap cycle from the tractor cab without stopping or dismounting.
Lower fuel cost
Eliminating a second tractor pass reduces per-bale fuel consumption significantly.
6. The Gearbox: Transmission Heart of the Integration System
The gearbox in a round baler integration system performs several functions simultaneously: it steps down PTO input speed from 720 rpm to the varied operational speeds needed by different working components, it allows the machine to turn on headlands without disconnecting drive, and it protects downstream components from shock loads when an oversize clump of material enters the pickup.
In the 9YG-2.24D S9000 series, a dual-joint (double cross-joint) transmission shaft was developed in-house to resolve a persistent problem in tractor-trailed balers: the driveshaft jamming or stuttering when turning tight headlands on small fields. The dual gearbox can articulate 90 degrees left and right from center, meaning power transmission is maintained at full turning lock without cutting PTO engagement. This single design improvement meaningfully increases field efficiency on irregular or small plots where frequent turning is unavoidable.
The gearbox housing in most commercial round balers is cast nodular iron (EN-GJS-500-7 equivalent) or fabricated steel with sealed oil bath lubrication. Gear teeth are typically case-hardened to 58–62 HRC. Operating temperatures must be maintained below 80°C under continuous load; exceeding this threshold accelerates lubricant breakdown and bearing wear. In integrated combinations, the secondary hydraulic circuit for the wrapper adds thermal load, so adequate gearbox oil capacity and, in some designs, an external oil cooler, are necessary for long operating days.
The torque safety mechanism is equally important. Integrated systems connect more driven components, meaning a blockage anywhere in the chain can cause a catastrophic over-torque event. Shear-bolt or friction-clutch torque limiters are placed at critical points — typically between the PTO shaft and the main gearbox input, and between the gearbox and the wrapper drive circuit — to absorb peak loads before gears, bearings, or welds fail. Replacing a shear bolt costs almost nothing; replacing a cracked gearbox housing or bent main frame does not.
7. Compatible Round Baler Models for Integrated Wrapping
Understanding a bale wrapper integration system means knowing which base machines support it. The following round balers from our product range are engineered with the hydraulic circuits, tailgate geometry, and ejection speed required to work efficiently with wrapper attachments. Each model’s technical parameters directly influence how quickly bales can be transferred, how consistent bale shape is, and how predictable the wrapping process becomes.
9YG-2.24D ラウンドベーラー(S9000 Transcend)
Bale φ1,300×1,400 mm · 40–100 bales/h · 55–100 kW · Dual-joint drive shaft · Sensor-controlled density
9YG-2.24D ラウンドベーラー(S9000クラシック)
Bale φ1,300×1,400 mm · 4,312 kg machine weight · Dual-side chain drive · H-type hydraulic fittings
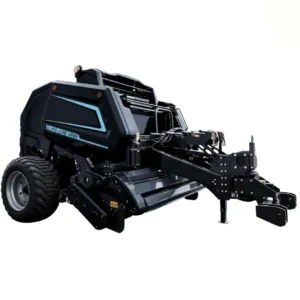
9YG-2.24D Round Baler (Transcend)
Pickup 2,240 mm · 18 rollers · 720 r/min PTO · Working speed 5–35 km/h · Auto net wrap
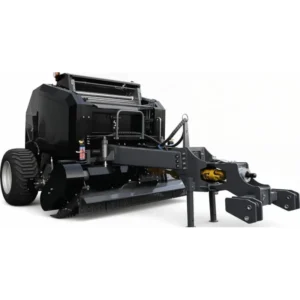
9YG-1.25 ラウンドベーラー
Bale 1,300×1,250 mm · ≥75 kW power · Interchangeable spring-tine / hammer-claw pickup · 40–100 bales/h
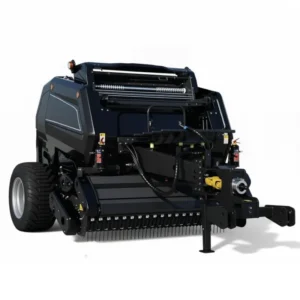
9YG-1.25A ラウンドベーラー
540–1,000 r/min PTO · Bale density 100–200 kg/m³ · Net 2,000×1.25 m/bale · 4,472 kg
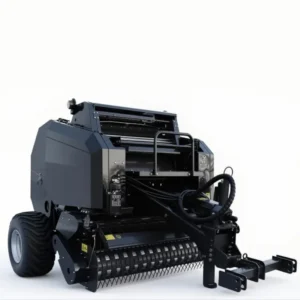
9YG-1.0 Round Baler (Small Round Baler)
48–80 kW · Bale φ1,100×1,000 mm · Small round baler for 40 hp tractor class · 2,640 kg
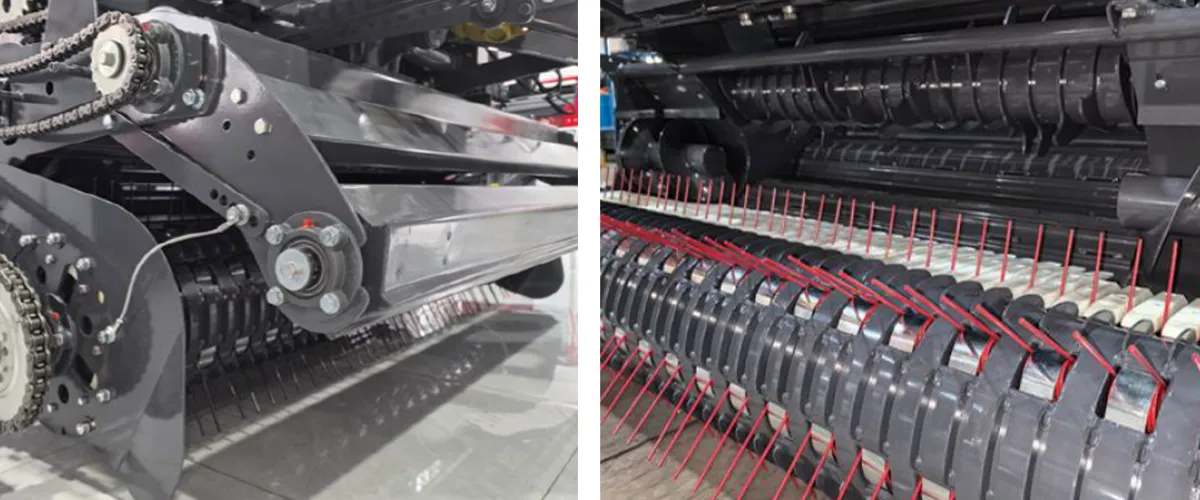
8. Key Technical Considerations When Selecting an Integrated System
Choosing the right bale wrapper integration configuration depends on several interacting variables: the range of crops you handle, the terrain you work on, your tractor’s horsepower and hydraulic flow, and the annual volume of bales you expect to produce. Getting these parameters right before purchase avoids the common situation where a machine is theoretically capable but practically under-powered for typical field conditions.
Comparative Model Specifications
| Model | Power (kW) | Bale Size (mm) | Output (bales/h) | ピックアップ幅 | Machine Weight (kg) |
|---|---|---|---|---|---|
| 9YG-2.24D S9000 Transcend | 55–100 | φ1,300×1,400 | 40~100 | 2,240 mm | 4,570 |
| 9YG-2.24D S9000 Classic | 55–100 | φ1,300×1,400 | 40~100 | 2,240 mm | 4,312 |
| 9YG-1.25 (Double) | ≥88.2 | 1,200×1,250 | 40–80 | 2,240 mm | 4,558 |
| 9YG-1.25A | ≥75 | φ1,300×1,250 | 40~100 | 2,150 mm | 4,472 |
| 9YG-1.0 (Mini Round Baler) | 48~80 | φ1,100×1,000 | 40~100 | 1,900 mm | 2,640 |
| 9YG-1.0C | ≥69.8 | φ1,000×1,250 | 40–80 | 2,400 mm | 3,198 |
9. Regulatory Requirements Across Key Markets
Agricultural machinery including round balers and integrated wrapper systems is subject to varying national and regional regulations. Understanding the compliance landscape is essential for procurement teams, importers, and farm owners alike.
韓国
In South Korea, agricultural machinery must comply with the Act on the Development, Management and Support of Agricultural Mechanization (농업기계화 촉진법), administered by the Ministry of Agriculture, Food and Rural Affairs (MAFRA). Balers and combined baling-wrapping machines fall under this legislation and must pass performance evaluation through the National Institute of Agricultural Sciences (농촌진흥청) before they are eligible for government purchase subsidies under the agricultural mechanization support program. Machinery that has not received certification cannot be listed on approved subsidy purchase lists, which significantly affects purchase economics for Korean farmers. Additionally, Korea’s Industrial Safety and Health Act (산업안전보건법) applies to PTO-driven implements, requiring guards on all power take-off shafts and rotating components when the machine is sold for commercial operation.
European Union (CE Marking)
Machines sold into EU member states, including round balers with integrated wrappers, must carry CE marking under Machinery Directive 2006/42/EC (and transitioning to Machinery Regulation (EU) 2023/1230). This requires a Declaration of Conformity, a technical file, and compliance with applicable harmonized standards including EN ISO 4254-7 (agricultural machinery — safety — harvesting machinery) and EN ISO 11684 (safety signs). The gearbox specifically must meet requirements under EN ISO 5673 for PTO drive shafts and EN 12965 for PTO drive shafts with universal joints. Failure to comply prevents lawful sale within the EU single market.
United States and Canada
In North America, agricultural equipment safety for commercial use is governed primarily through ASABE (American Society of Agricultural and Biological Engineers) standards, particularly ASABE S318 (safety for agricultural equipment) and ASABE S207 (PTO definitions). OSHA regulation 29 CFR 1928 covers agricultural operations and requires point-of-operation guarding on PTO-driven implements used by employed labor. Canada’s CCME and provincial bodies impose similar requirements. Environmental regulations affecting silage plastic — particularly the disposal of used stretch film — are increasingly being codified; several Canadian provinces now require farm plastic recycling participation.
Russia and CIS Markets
Agricultural machinery sold in Russia must carry GOST R certification (Государственный стандарт) and comply with the Technical Regulations of the Customs Union (TR CU 010/2011 — machinery safety). Machines operating in Kazakhstan and Belarus also fall under EEU (Eurasian Economic Union) technical regulations TR EAEU 010/2011. Gearbox oil standards in these markets typically reference GOST 23652 (gear oils for agricultural machinery), and compliance with these specifications is expected in warranty and service agreements.
Mongolia
Mongolia’s agricultural mechanization is supported through the Ministry of Food, Agriculture and Light Industry, with equipment subsidies administered under the National Program for Livestock and Agriculture Development. Imported machinery must clear Mongolian Customs and meet MNS (Mongolian National Standard) requirements where applicable. As standards infrastructure in Mongolia is still developing, ISO certification (particularly ISO 9001 quality management) is often accepted as a proxy compliance indicator by Mongolian procurement authorities.
10. Why Wrapping Speed Directly Affects Silage Fermentation Quality
Many operators focus on the mechanical aspects of integration systems without fully appreciating the fermentation science that drives the urgency. Silage making is a managed anaerobic fermentation process: lactic acid bacteria (LAB) naturally present on plant material consume water-soluble carbohydrates and produce lactic acid, dropping pH from around 6.5 to below 4.5. This acidification preserves the forage by inhibiting the growth of spoilage organisms including clostridia, molds, and enterobacteria.
The critical condition for successful fermentation is the rapid exclusion of oxygen. Every minute that a formed bale sits exposed to air before wrapping gives aerobic bacteria — particularly those that break down sugars before LAB can access them — additional time to consume fermentable substrate. This reduces the eventual lactic acid concentration and raises final pH, producing silage that spoils faster when the bale is opened and that delivers lower energy density to ruminant livestock.
Research by the Korean Rural Development Administration (농촌진흥청) has documented Italian ryegrass silage DM losses of 2–7% per day of aerobic exposure before sealing, depending on moisture content and ambient temperature. At harvest-season Korean temperatures of 20–30°C, this is a highly significant loss window. An integrated bale wrapper system that seals bales within two to five minutes of formation effectively closes this window, protecting both forage quality and the economic value of the crop.

11. Maintenance Requirements and Extending Service Life
An integrated bale wrapper system has roughly double the mechanical complexity of a standalone round baler, and maintenance discipline is correspondingly more important. Daily service intervals during peak harvesting season should include chain lubrication on all drive circuits — pickup, pre-chamber, baling chamber, and wrapper drive — as well as inspection of all hydraulic hose connections for weeping or chafing. The axial-flow feed rotor and feeder roller clearances should be checked weekly, as crop debris accumulation alters effective clearance and can cause uneven chamber filling that produces misshapen bales incompatible with wrapper geometry.
The gearbox oil level deserves particular attention in integrated systems because the hydraulic demand of the wrapper circuit can mask slow gear oil consumption if the two systems share a common reservoir. If they are separate circuits — the more common arrangement — each reservoir should be checked independently. Gear oil change intervals for sealed baler gearboxes typically fall at 200–250 operating hours or annually, whichever comes first. Using the wrong viscosity grade — commonly mistaking the ISO VG 150 gear oil specified for these applications for the lighter hydraulic oil used in the wrapper circuit — is a recurring source of premature gearbox failure in the field.
Round baler parts most commonly subject to wear include the spring tines on the pickup reel, the rubber-tipped cam-less pickup lugs (where fitted), the chain side-plates and rollers in the compression circuit, and the net-wrap knife assembly. Maintaining a stock of these round baler parts allows on-farm repair that avoids multi-day downtime during the critical harvest window. The wrapper section’s primary wear items are the film-roll holder bearings, the film pre-stretch rollers, and the turntable or satellite arm bearings — all standard items available from agricultural parts suppliers.
Frequently Asked Questions
編集者: PXY