Cotton Stalk Baling | Anti-Clog Technology | Round Baler Application
A technical and practical guide for cotton-growing regions evaluating round baler machines for post-harvest stalk management — covering the engineering principles that prevent clogging, the material systems that resist woody stalk wear, regulatory obligations in key markets, and the machine configurations best suited to cotton residue programs.
Cotton Stalk Baling
Anti-Clog Engineering
1. Cotton Stalk Baling: The Challenge That Exposes Baler Design Quality
Of all the crop residues that a round baler machine is asked to handle, cotton stalks consistently produce the most severe test of the machine’s anti-clog design, feeder system geometry, and component wear resistance. Unlike straw residues — which are flexible, relatively uniform in cross-section, and flow predictably into a baler’s compression chamber — cotton stalks combine rigidity with fibrous strand attachment at the nodes, creating a material that simultaneously resists being bent into the compression chamber and wraps aggressively around any rotating component it contacts. After mechanical picking, the stalks are typically still rooted in dry, compacted soil, which means significant breakage stress at the base when the baler’s pickup engages them. The resulting debris mix — broken stalk segments, cotton fiber strands, dried leaf fragments, and soil fines — is one of the most challenging material streams a round baler application can encounter.
The question of clogging is not simply about inconvenience. In commercial cotton production regions — from the Xinjiang basin to Uzbekistan’s Fergana Valley, from the Indus plain to the cotton-growing areas of South Korea’s Gyeongnam coast — a baler that blocks repeatedly during the narrow post-harvest window reduces field throughput, increases operator labor, and risks missing the window entirely. Understanding how a well-engineered round baler prevents these blockages at the mechanical level is the starting point for specifying the right machine for a cotton stalk management program. This guide covers that engineering in detail, then connects it to product specifications, regulatory context, and practical operational guidance.
2. Why Cotton Stalks Cause Clogging in Conventional Round Balers
To understand what prevents clogging, it helps first to understand what causes it in machines not designed for this crop. Cotton stalks after mechanical picking stand at 0.8–1.4 m height, with a main stem diameter of 12–25 mm at the base and a branching structure that creates a dense, interlocking canopy of lateral stems. When a conventional cam-track pickup assembly engages these stalks, several failure modes become likely. The first is tine deflection without pickup: a spring tine designed for flexible hay stems may deflect against a rigid cotton stem rather than gripping and lifting it, leaving material in the field. The second is node wrapping: when a cotton stalk does enter the feeder system, the nodal protrusions along the stem create anchor points around rotating components — feeder rollers, auger flights, and pickup tine bar carriers — initiating the progressive wrapping that leads to a full blockage within 3–5 minutes if not immediately cleared.
The third failure mode is chamber entry jamming at the compression chamber inlet. Cotton stalks that break during pickup produce segments of varying length from 150 mm to 600 mm. Short segments feed erratically and tend to orient perpendicular to the feed direction, creating a mat at the chamber inlet that progressively blocks material flow. Longer segments, by contrast, feed more predictably but require greater feeder force to redirect from the linear pickup direction into the circumferential rotation inside the chamber. Machines designed for hay — which is short-cut, flexible, and easily redirected — typically lack the feeder geometry and force margin to handle this redirection reliably for woody cotton stalk segments.
Standard spring tines designed for flexible hay deflect rather than grip rigid cotton stems with 12–25 mm base diameter. Specialized tine geometry or hammer-claw pickup is needed for consistent cotton stalk engagement.
Cotton stalk nodes act as snag points on rotating components. Without anti-wrap geometry on feeder rollers and tine bar carriers, progressive wrapping leads to full blockage within minutes of onset.
Broken stalk segments (150–600 mm) orient erratically at the compression chamber inlet. Multi-stage feeder systems with active crop control prevent the inlet mat formation that causes blockage in single-stage feeders.
Residual cotton fiber attached to stems at nodes wraps around rotating shafts and bearings when stalks are processed. Shaft diameter, seal design, and clearance geometry at bearing locations determine how quickly fiber accumulates to a damaging level.
3. Manufacturing Structure: What Enables Anti-Clog Performance
A round baler machine capable of processing cotton stalks without repeated clogging is distinguishable from a standard hay baler at every stage of the crop flow path — from pickup to compression chamber to net wrapping. The following section examines each structural subsystem and explains how its design addresses the specific clogging mechanisms identified above. The product specifications referenced here are drawn from the 9YG round baler series, which covers configurations from compact small round balers at 48 kW to heavy-capacity models at 100 kW.
Pickup Mechanism for Rigid Stalks
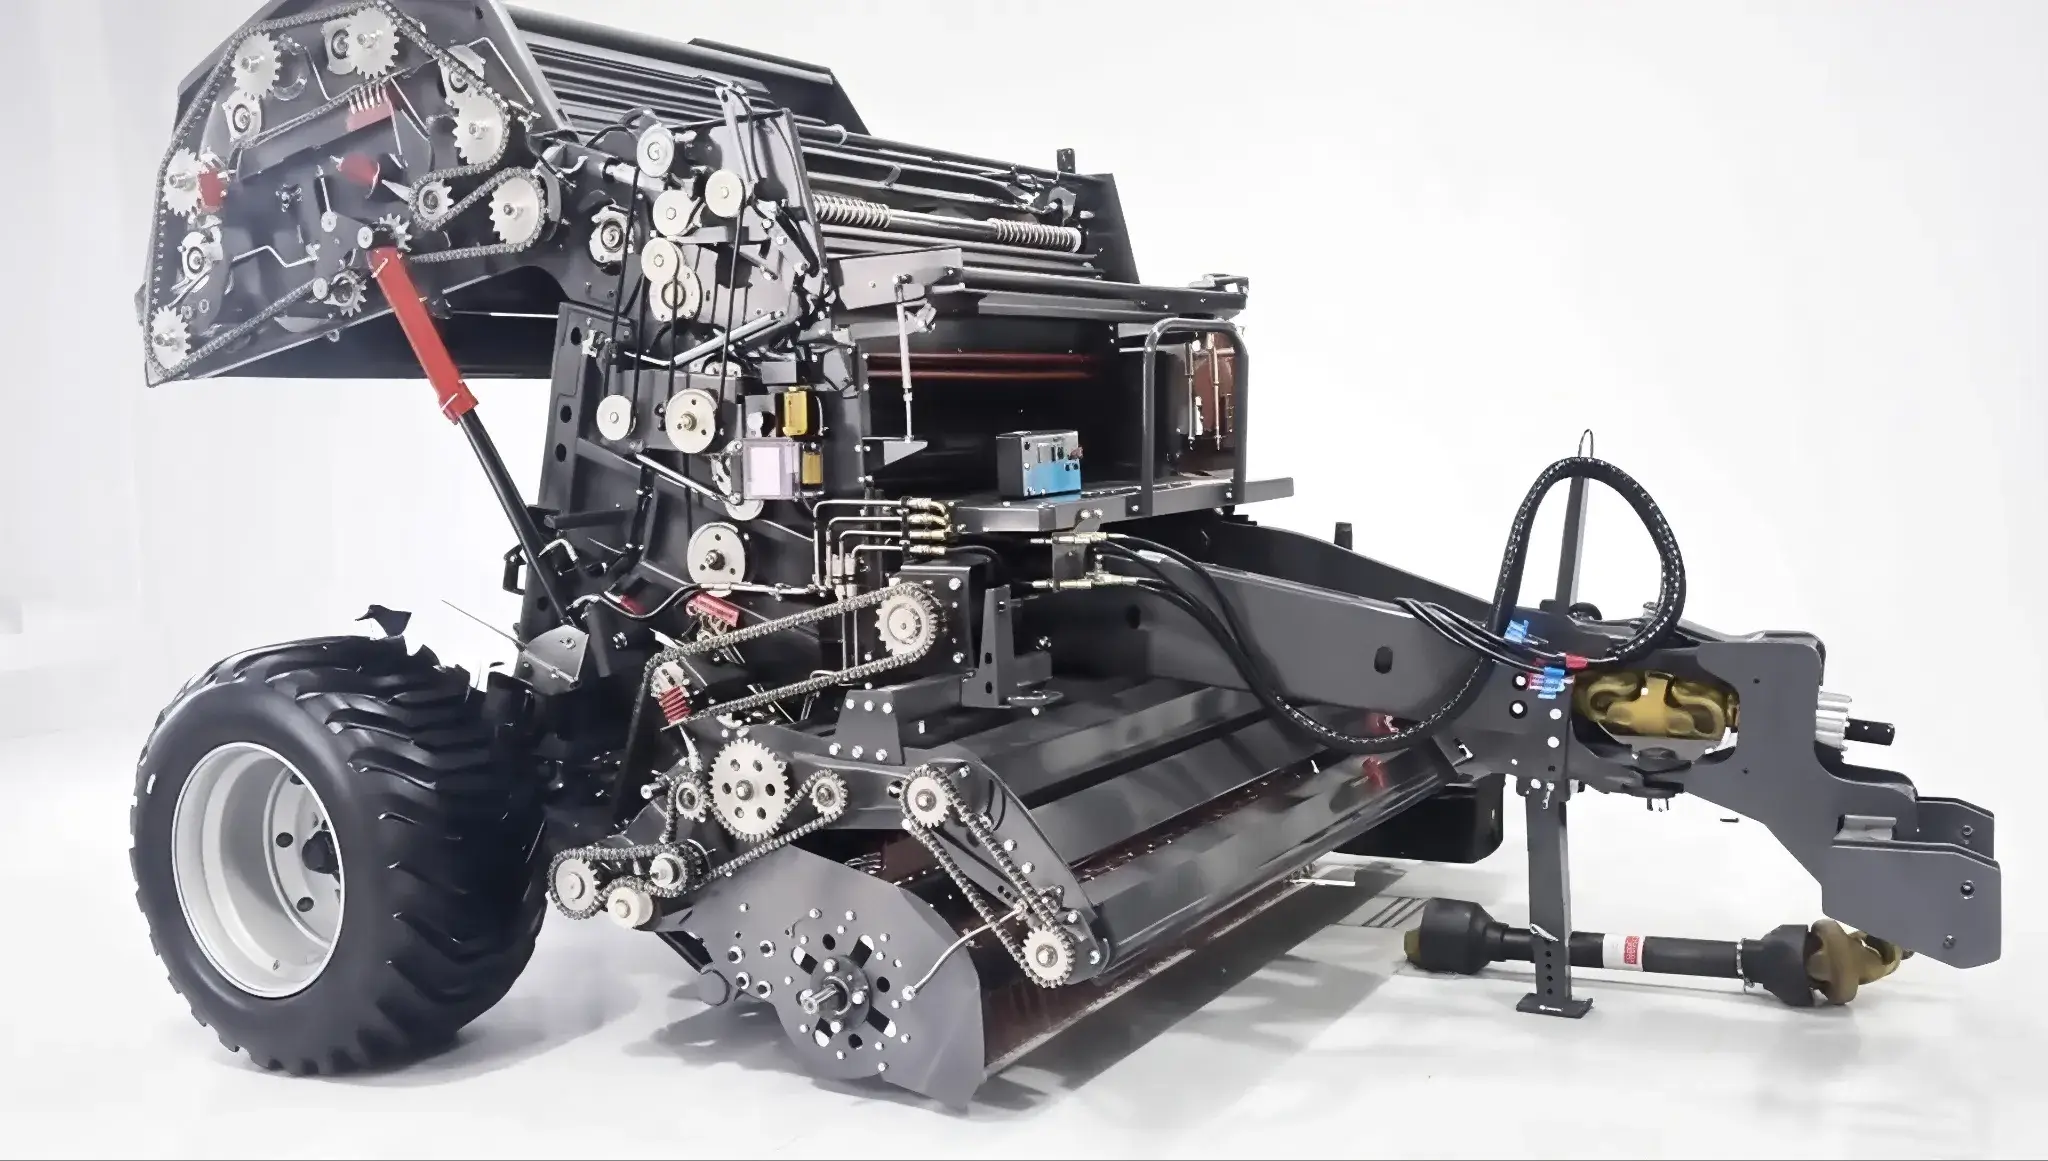
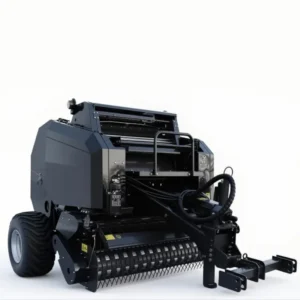
The pickup mechanism is the entry point for all clogging problems. For cotton stalks after mechanical picking, the hammer-claw pickup configuration provides materially better performance than standard spring-tine designs. The hammer-claw operates with a downward-striking, raking motion that physically breaks loose partially rooted stalks, separates interlocked branching stems, and delivers them to the feeder assembly in a more controlled flow than a spring-tine sweep can manage. The 9YG-1.0C model, for instance, features a 2,400 mm hammer-claw pickup with 20 claw units — a wide working width that ensures thorough stalk collection across the full cut width of a standard mechanical cotton picker. The 9YG-1.25 series further offers an interchangeable pickup system where the spring-tine set can be exchanged for the hammer-claw configuration, giving cotton-growing operations the flexibility to configure the same machine for both wheat straw (spring-tine) and cotton stalk (hammer-claw) programs without acquiring a second machine.
Feeder System: The Anti-Clog Core
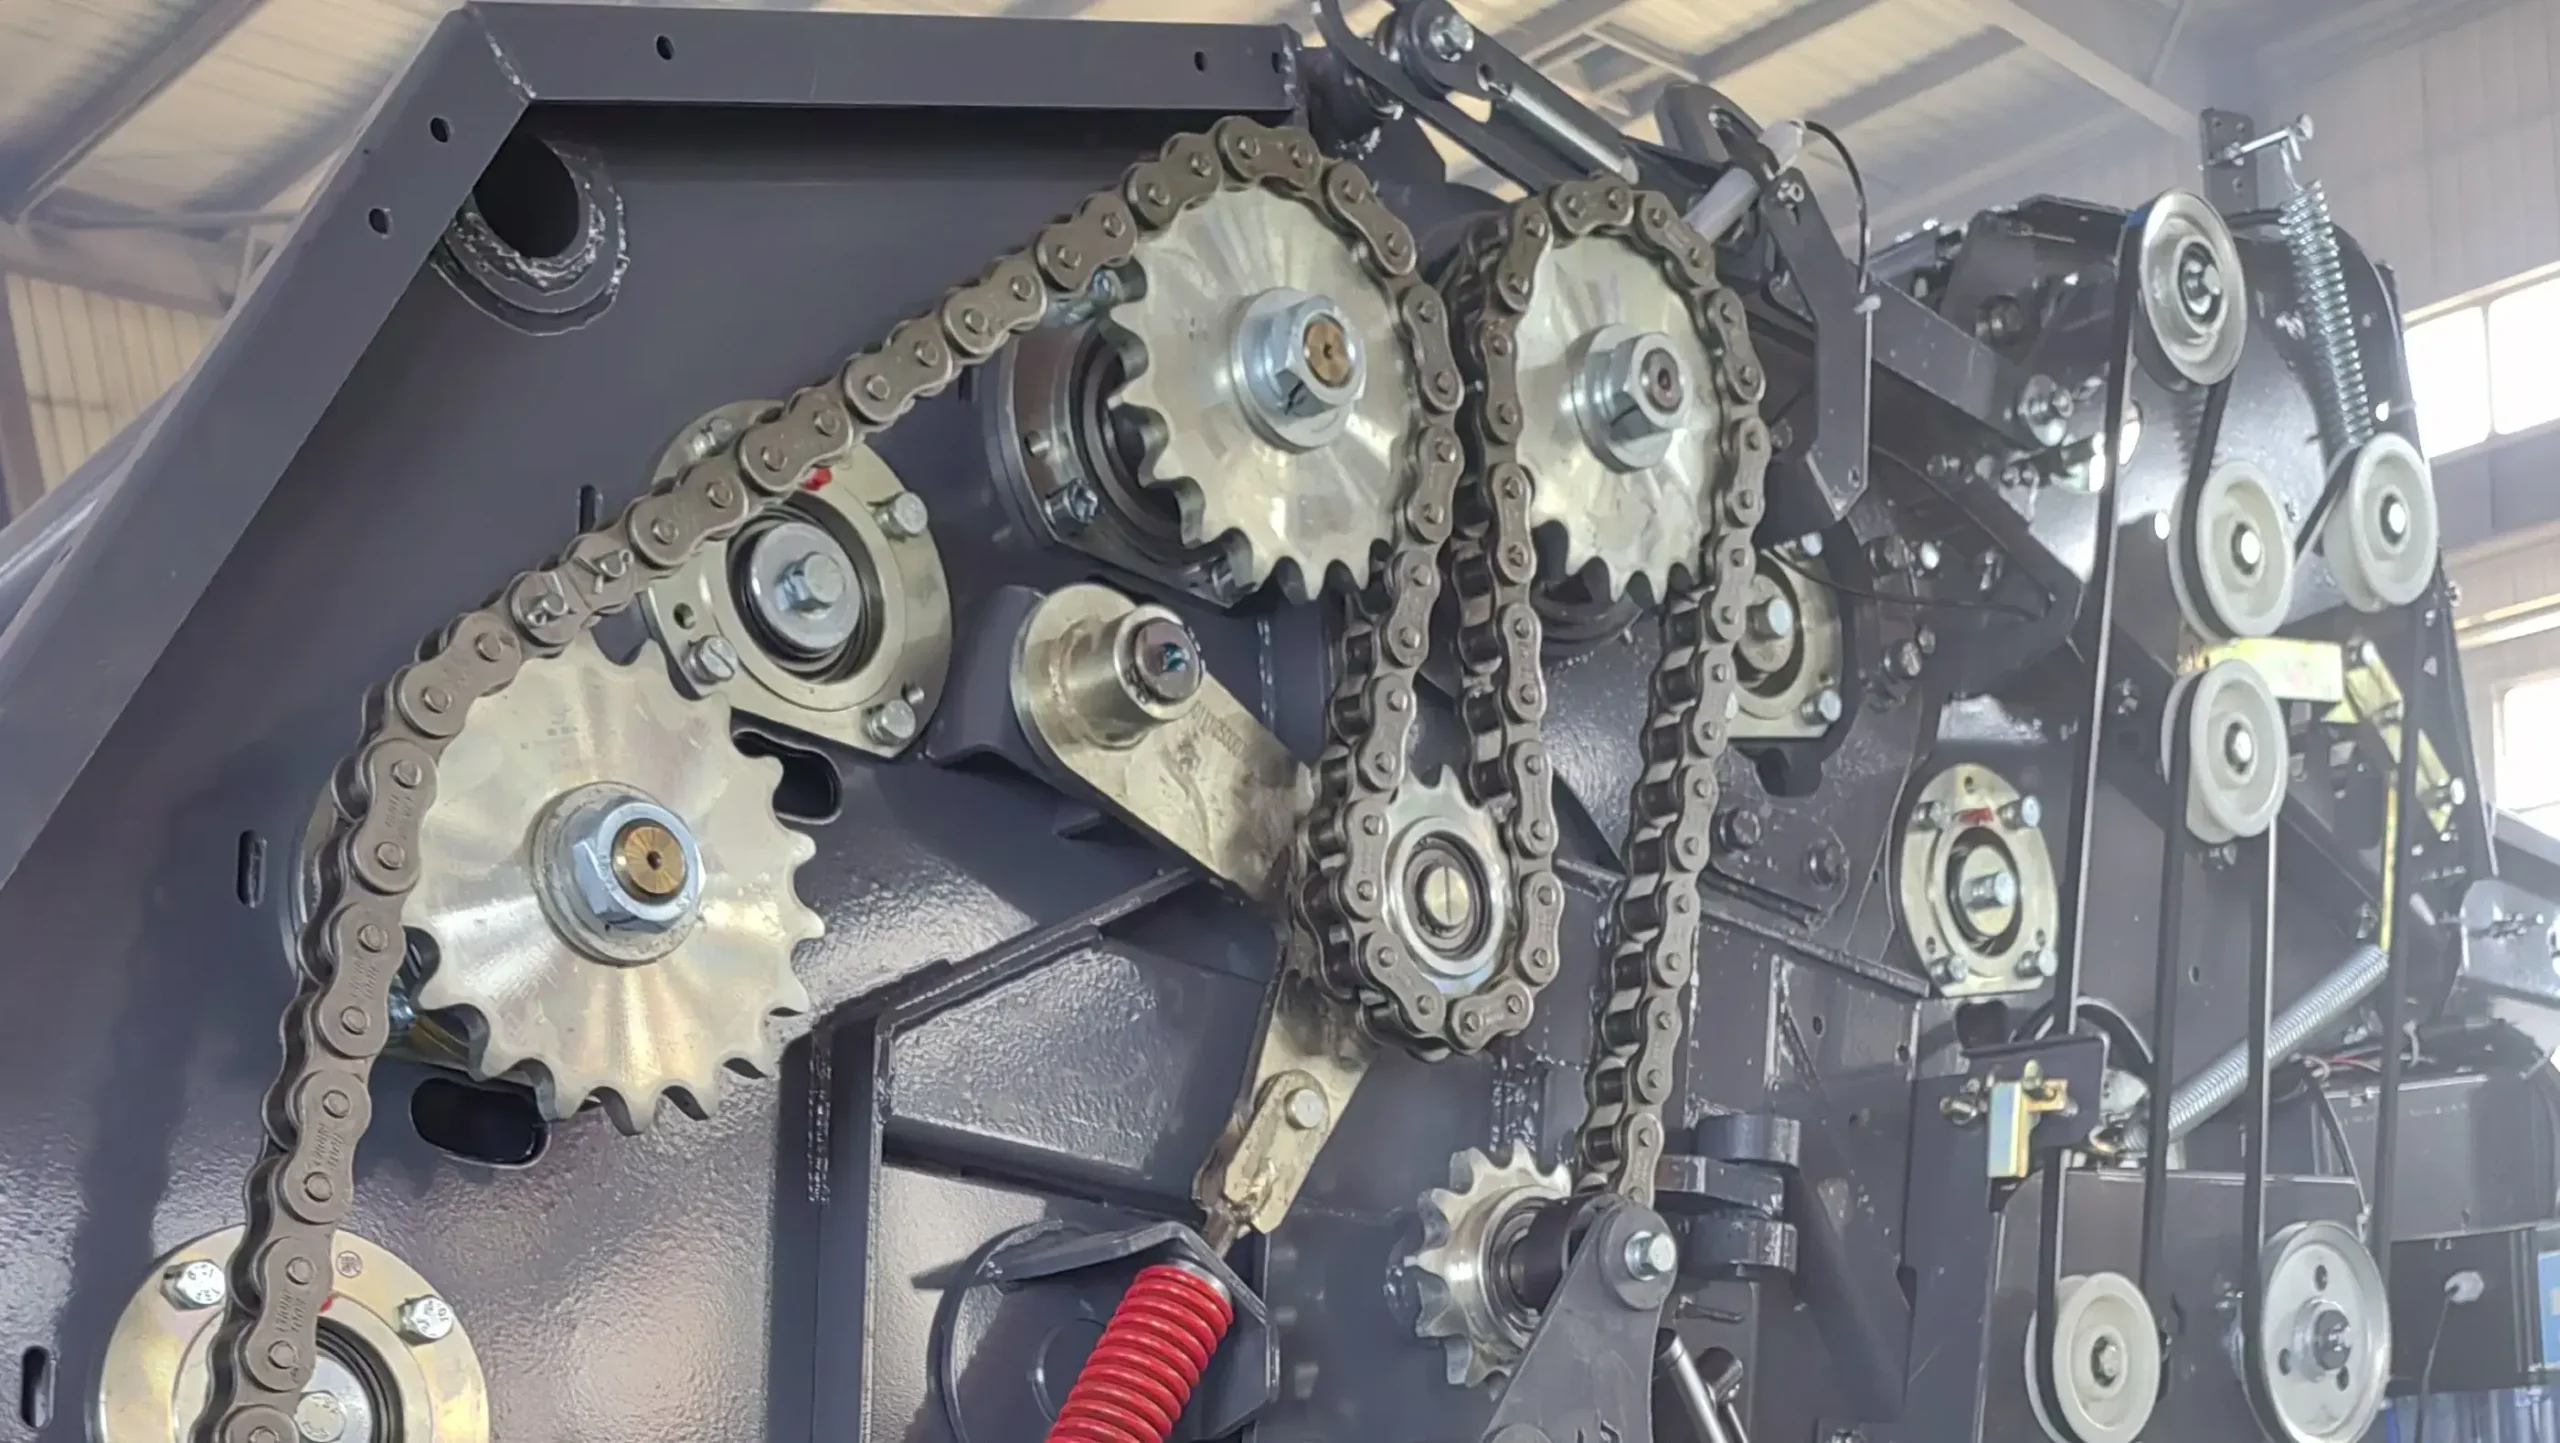
The feeder system is where the difference between a round baler application that handles cotton successfully and one that clogs repeatedly is most clearly visible. The 9YG series uses what the manufacturer calls an axial-flow semi-forced feeding mechanism on its base models — a camless design that eliminates the cam track found in conventional pickup assemblies. The cam track is a notorious blockage point in cotton stalk applications: stalk segments and fiber strands accumulate in the cam follower groove, progressively restricting cam rotation until the pickup jams. The camless design in the 9YG-1.0 and 9YG-2.24D series removes this failure mode entirely, which the manufacturer claims reduces the probability of feed blockage by enough to nearly double effective operating efficiency compared to traditional cam-track designs. On the 9YG-1.25, the auger-plus-roller-plus-drum three-element feeder provides forced crop control at the intake: the helical auger centrally consolidates material, the toothed roller breaks up bunched cotton stalk segments before chamber entry, and the drum provides the final directional acceleration into the compression chamber. This staged, forced intake prevents the erratic orientation of broken stalk segments that causes inlet jams in simpler feeder designs.
Compression Chamber Design for Woody Material
Inside the fixed compression chamber, the bale is formed by 16 or 18 steel rollers (Ø222 mm each) arranged in a closed ring. For cotton stalk applications, the roller surface profile is a critical detail. The spiral groove pattern on the roller surface — standard across the 9YG compression chamber design — maintains rotational grip on rigid stalk fragments that would slide on a smooth roller surface. This grip is what keeps the bale rotating inside the chamber rather than stalling against the inlet. Stall is the compression chamber equivalent of a feeder clog: when the bale stops rotating, incoming material piles against the stationary mass rather than integrating into it, and the chamber fills with uncompressed material within seconds. The 18-roller configuration used in the 9YG-1.25, 9YG-2.24D, and related models provides more circumferential contact points than a 16-roller layout, distributing the rotational force across a larger surface area and reducing the per-roller load that might otherwise stall the bale in dense cotton stalk conditions.
Net Wrapping in Cotton Fiber Conditions
The net wrapping mechanism presents a secondary clogging risk in cotton stalk applications that is often overlooked: residual cotton fibers from the post-harvest stalk field can accumulate in the net knife mechanism, eventually preventing clean cutting and causing wrapping failures. Machines with a well-sealed net guide path and a positive-cut knife design — rather than a friction-cut or tear-off design — are significantly less susceptible to fiber accumulation in the cutting zone. The automatic net wrapping system across the 9YG range uses this positive-cut mechanism, and net consumption is standardized at 2,000 m per bale across most models (with bale width variants from 1.0 m to 1.4 m depending on model). In cotton stalk service, net wrap is strongly preferred over twine both because fiber fragments on the bale surface interfere with twine loop placement and because the net surface better contains loose cotton fiber that would otherwise escape from a twine-bound bale during transport.
4. Material System: Component Specifications for Cotton Stalk Service
Cotton stalk baling creates a material wear environment significantly different from hay or even rice straw. Dried cotton stalks have a Brinell hardness at the woody stem zones that exceeds most grasses, and the fibrous strand content at nodes creates a wrapping medium that is more damaging to shaft seals than silica-laden straw. The material specifications in the 9YG production series respond to these conditions through the following component choices.
5. Round Baler Gearbox Design for Cotton Stalk Torque Demands
The round baler gearbox is under significantly greater torque stress in cotton stalk applications than in hay or even rice straw operations. This is because the compression of woody material inside the fixed chamber requires the roller array to generate higher radial force against a stiffer bale core — particularly in the early bale-building phase when the core is being established from rigid stalk fragments. At this stage, the gearbox must transmit peak torque without the demand modulation that occurs naturally in flexible crop baling, where the incoming material continuously compresses and reduces peak loads. The practical consequence is that gearbox oil temperature rises faster in cotton stalk service, and the risk of gear surface micropitting — a progressive wear mode caused by sustained high tooth-face stress — is elevated compared to grass crop applications.
The 9YG-2.24D S9000 series addresses this with its twin-axle heavy-duty gearbox rated at 1,000 Nm maximum input torque, housed in a nodular iron (QT450) casing that provides superior vibration damping compared to grey iron alternatives. The PTO input speed of 720 r/min is standard across the 9YG range, except the 9YG-1.25A which accepts 540–1,000 r/min — a useful range for operations where available tractor PTO speed varies across different machines in a mixed fleet. For cotton stalk operations specifically, the key gearbox specification questions to ask any round baler manufacturer are: what is the rated continuous input torque (not just peak), what is the oil capacity and recommended change interval under heavy-duty service, and is the gearbox housing fitted with a temperature-sensitive oil cap or sight glass that allows condition monitoring without a full disassembly.
6. Round Baler Models for Cotton Stalk Applications
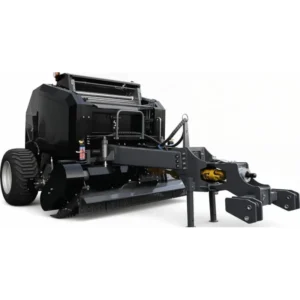
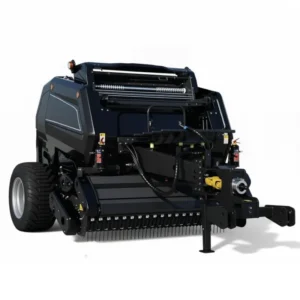
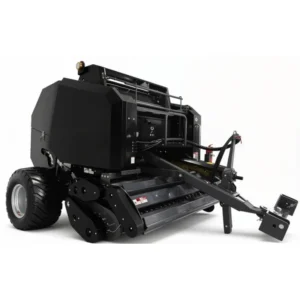
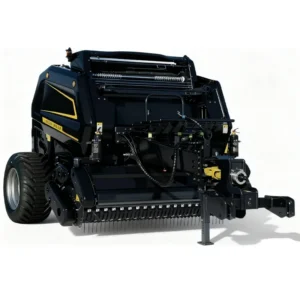
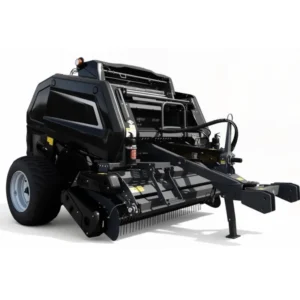
The following models cover the full operational range from compact round baler machines at 48 kW to heavy-capacity configurations at 100 kW — all with the anti-clog feeder technology and heavy-duty chain specifications suited to woody crop residue processing.
7. Cotton Stalk End Uses and What They Require from the Bale
The round baler application for cotton stalks has grown across multiple downstream markets, and the bale specification requirements vary meaningfully between them. Biomass energy plants that co-fire cotton stalks with coal are typically the largest-volume buyer in Central Asian and East Asian cotton-growing regions. These plants generally accept a wide density range (80–200 kg/m³) but require consistent bale dimensions for automated feed handling systems. Cotton gin residue compost programs prefer lower-density bales that allow faster composting aeration. Mushroom cultivation substrate processors — a smaller but higher-value market in South Korea’s agricultural areas — require clean bales with minimal soil contamination and cotton fiber content below a specified threshold.
For Korean cotton-growing operations in Gyeongnam and Jeolla, the primary downstream channel is typically biomass energy under Korea’s Renewable Portfolio Standard (RPS), which requires power producers to source a percentage of electricity from renewable sources. Cotton stalk bales qualify as an agricultural biomass fuel under the RPS framework. This means that the baling operation’s output — bale dimensions, density, moisture content at baling, and net wrap integrity — must meet the specifications of the contracted biomass plant, making sensor-controlled density monitoring a commercially relevant feature rather than a convenience option.
8. Regulatory Framework: Cotton Stalk Burning Bans and Equipment Standards
Cotton stalk burning has historically been common practice in major cotton-growing regions, but regulatory pressure has intensified substantially over the past decade as governments across Asia and Central Asia target agricultural residue burning as a PM2.5 source. Understanding this regulatory context is essential for buyers evaluating the business case for a round baler machine investment in cotton stalk management programs.
South Korea — RPS Biomass and Burn Restrictions
South Korea’s Clean Air Conservation Act (대기환경보전법) prohibits open-field burning of agricultural residue, including cotton stalks, during designated periods enforced at the provincial level. Violations carry administrative fines and can affect a farm’s eligibility for agricultural support payments. On the positive side, the Renewable Portfolio Standard (신재생에너지 공급의무화제도, RPS) creates a commercial market for agricultural biomass including cotton stalks, with verified bale supply qualifying for RPS credit trading. Machinery used for stalk collection may qualify for the Rural Development Administration (농촌진흥청, RDA) low-interest equipment financing program at 1.5–2.0% per annum, subject to technical inspection under KS B 6007 and the Agricultural Mechanization Promotion Act (농업기계화 촉진법).
Uzbekistan and Central Asia — Major Cotton Stalk Markets
Uzbekistan is one of the world’s largest cotton producers, with approximately 1.0–1.2 million hectares under cotton production annually. The government’s 2019–2025 cotton sector modernization program includes specific provisions against open straw and stalk burning, and promotes mechanical residue collection as a soil conservation and air quality measure. Cotton stalk baling for biomass energy is supported under Uzbekistan’s renewable energy framework legislation (Law on Renewable Energy Sources, 2019). Machinery safety requirements for agricultural equipment in Uzbekistan follow GOST standards adapted from the former Soviet system, with GOST R 53504 and related standards covering agricultural machinery safety. Importers should confirm GOST certification status and, for EU-origin equipment, whether the EAC (Eurasian Conformity) marking is also required for customs clearance.
European Union — Cotton-Growing Regions
Cotton is grown commercially in the EU in Greece (Macedonia and Thessaly) and Spain (Andalusia) — together producing approximately 300,000–350,000 tonnes of cotton annually. Agricultural residue burning in these regions is restricted under national implementing regulations of EU Directive 2008/50/EC on ambient air quality, and under the CAP Good Agricultural and Environmental Conditions (GAEC) requirements that condition subsidy payments on environmentally responsible residue management. Agricultural machinery entering Greek or Spanish markets must carry CE marking under Machinery Directive 2006/42/EC. The applicable harmonized standard is EN 703 (crop harvest and processing machinery) alongside EN ISO 11684 for safety signs and EN 12965 for PTO driveshafts.
India — Cotton Stalk Burning Prohibition Progress
India is the world’s largest cotton producer by area, and cotton stalk burning has historically been widespread in Maharashtra, Gujarat, Telangana, and Andhra Pradesh. The National Green Tribunal (NGT) has issued orders prohibiting agricultural residue burning in multiple state jurisdictions, and state pollution control boards in Maharashtra and Gujarat have implemented monitoring programs. The Central Institute of Agricultural Engineering (CIAE) under ICAR has promoted cotton stalk baling as a mechanical alternative, with subsidy support available under the Sub-Mission on Agricultural Mechanization (SMAM) program administered by the Ministry of Agriculture and Farmers’ Welfare. Machinery imported for agricultural use in India requires BIS certification for applicable standards under the Agricultural Machinery Act and Weights and Measures Act frameworks.
9. Compatible Drive Components: Agricultural PTO Shaft and Drive Chain
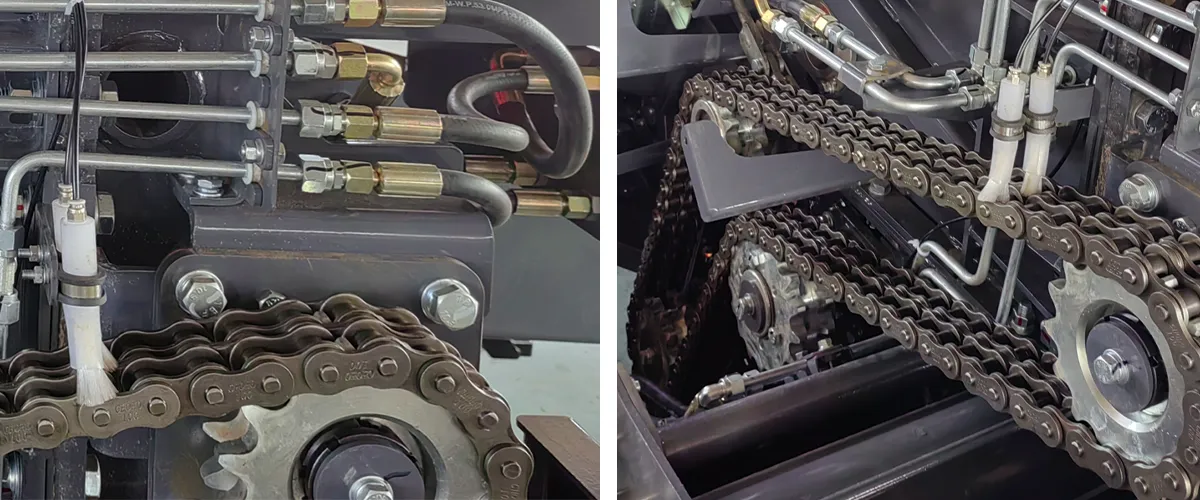
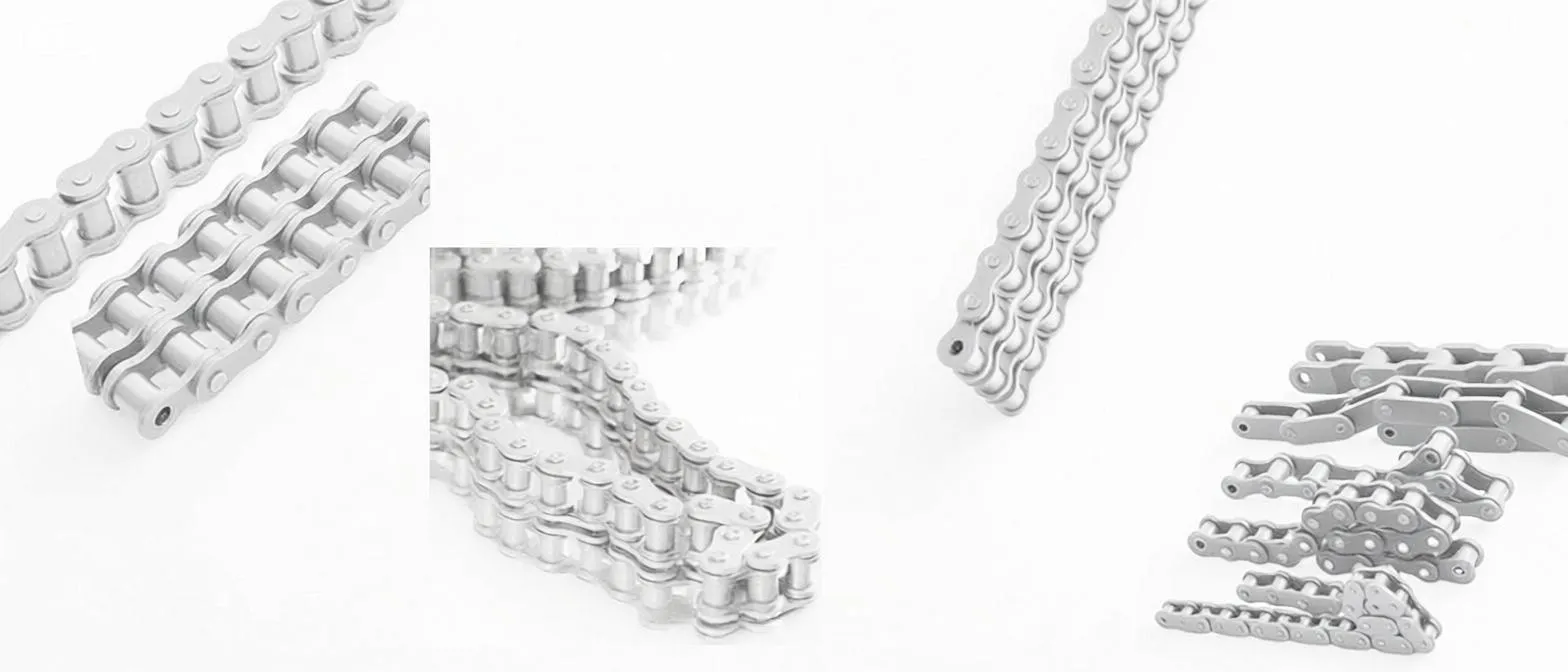
In cotton stalk applications where peak drivetrain torque is higher than in grass crop baling, specifying a purpose-rated Agricultural PTO Shaft for round balers is a meaningful reliability upgrade. Generic PTO shafts rated for standard hay applications are frequently underspecified for the sustained high-torque demand of cotton stalk bale core formation, and they fail through inner tube wear or cross-joint bearing fatigue typically within 200–300 operating hours in cotton stalk service. A shaft rated for the baler’s maximum PTO input torque with a safety factor of at least 1.5 provides adequate margin for the torque spikes that occur during rooted stalk engagement. Agricultural chain for the feeder and chamber systems should be sourced to the 16A and 20A specifications used in the factory configuration — substituting lighter chain grades as a cost saving measure produces false economy when chain failure stops the machine at the peak of the cotton harvest window.
PTO shafts purpose-engineered for round baler torque profiles. Overrunning clutch options available for cotton stalk shock-load protection. 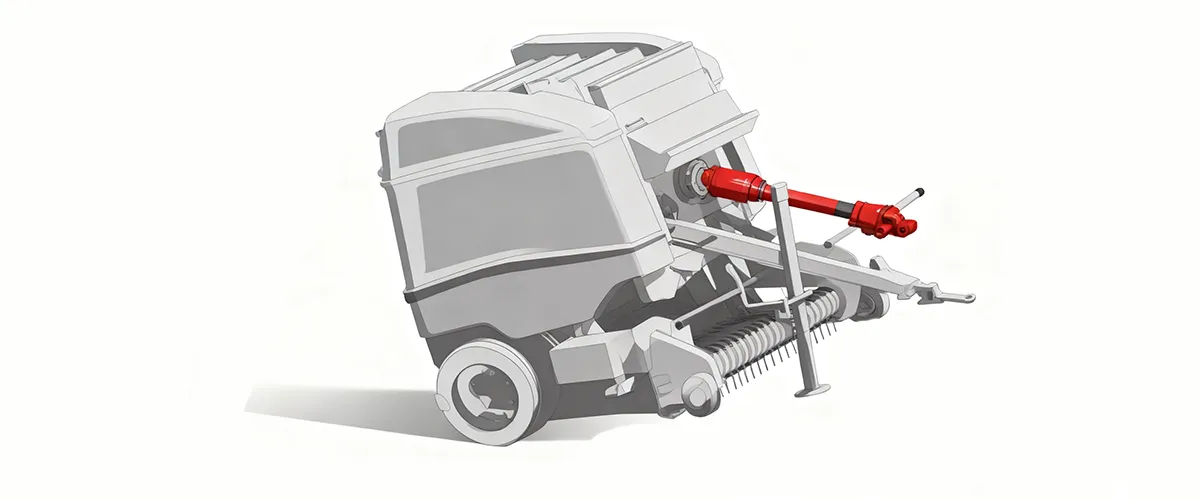
Heavy-duty roller chain sets in 16A and 20A specifications for 9YG series feeder and chamber drive systems. Surface-hardened pins for extended service in abrasive woody stalk environments. Sourced as factory-matched kits by baler model for dimensional accuracy.
10. Practical Operating Guidance for Cotton Stalk Round Baling
Getting consistent, clog-free performance from a round baler in cotton stalk conditions requires a few operational adjustments relative to grass crop baling that are often not covered in the standard machine manual. The first concerns ground speed: in cotton stalk applications, a lower working speed of 4–10 km/h — compared to 10–20 km/h for hay — is recommended during the initial passes when stalk volumes are highest. Slower speed reduces the instantaneous intake rate and gives the feeder system time to process each stalk section before the next one arrives. As the windrow is cleared and stalk volumes decrease, speed can be increased progressively. The second concerns pickup height: for partially rooted cotton stalks, the pickup should be set at or below the minimum safe-ground clearance for the terrain, allowing the hammer claws to engage the stalk base as close to the root as possible. Higher pickup settings — appropriate for windrowed hay — leave short stalk sections in the field and increase the proportion of irregular stalk segments that create inlet jams.
The third operational adjustment concerns daily maintenance during the cotton stalk season. Cotton fiber strands accumulate around the feeder shaft locations faster than any other crop residue. At minimum, these should be manually cleared from all rotating shaft locations at the end of each operating day — a 20–30 minute procedure that prevents the overnight drying and compaction of fiber wraps that makes them significantly harder to remove. Chain tension should be checked every 20–25 operating hours rather than the standard 30-hour interval recommended for hay, since the higher peak torque in cotton stalk baling causes faster chain elongation. A seasonal pre-maintenance kit should include at minimum one full set of pickup claws or tines (depending on configured pickup type), one full feeder chain set, and all hydraulic seal kits for the tailgate cylinders.
Frequently Asked Questions
Redaktor: PXY